EasyDoc WeldingProcedure qualification
Welding procedure qualification software

Welding procedure qualification to EN ISO 15614-1

Prepare the welding procedure qualification record (WPQR) from the welded test piece, automatically calculate the qualification ranges and the test plan, and get the record ready for the examiner's assessment.

Procedure qualification modules by standard

Each standard defines its own essential variables and procedure qualification ranges. Each module applies its rules, with the same company account you already use for welder WPQs.

01 · EN

WPQR to EN ISO 15614-1

Welding procedure qualification record for arc and gas welding of steels and nickel alloys. Levels 1 and 2, butt, fillet and branch joints, and up to three processes per procedure.

Open EN ISO 15614-1 module → ▶ Watch the demo video
02 · ASME

PQR and WPS to ASME IX

Procedure qualification record (PQR) and WPS to ASME BPVC Section IX for pressure vessels, boilers and piping. Groove or fillet test coupon, up to three processes (SMAW, GTAW, GMAW, FCAW, SAW) and supplementary essential variables when the code requires toughness.

Open ASME IX module → ▶ Watch the demo video
03 · AWS

PQR and WPS to AWS D1.1

Procedure qualification record (PQR) and WPS to AWS D1.1/D1.1M:2025 for structural steel. Groove or fillet test coupon, up to three processes per procedure and qualification ranges applied according to the code.

Open AWS D1.1 module → ▶ Watch the demo video

What the EN ISO 15614-1 module calculates

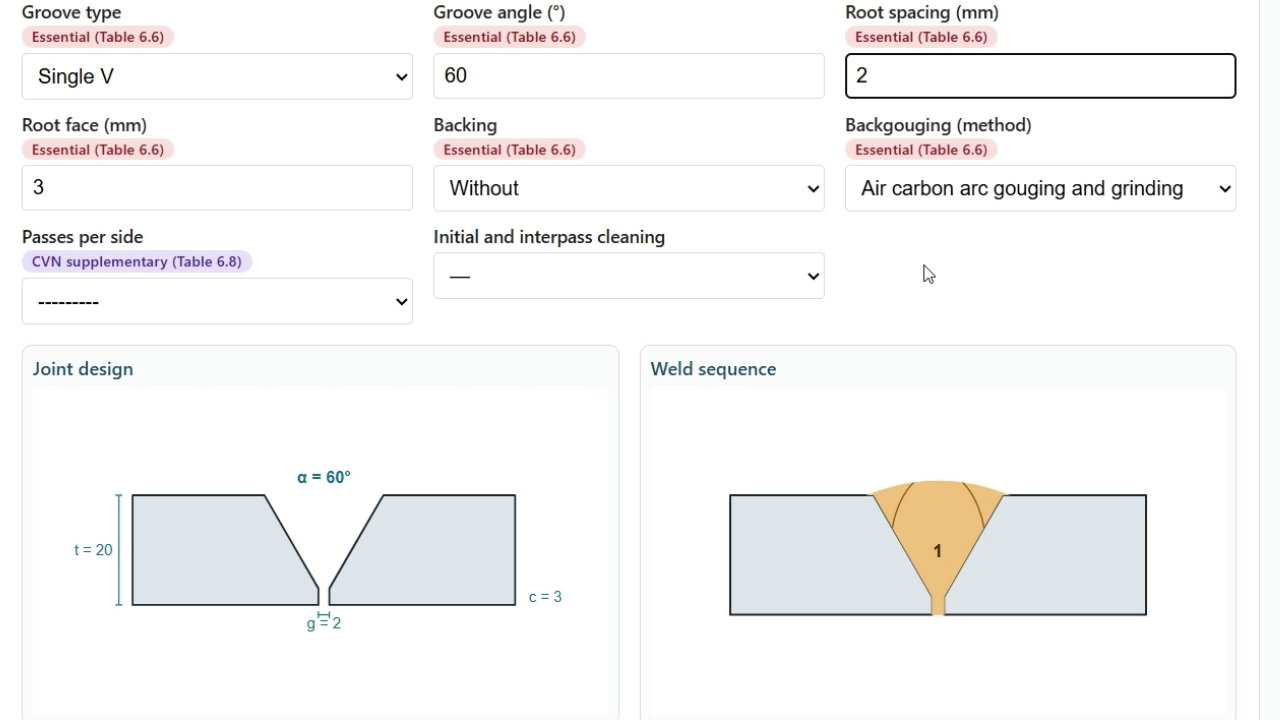
As you enter the test piece data, the module shows live the qualified range of each variable and the tests required by the standard.

Parent materialGroups and subgroups to ISO/TR 15608 and dissimilar material combinations.
Thickness and diameterRange of parent material thickness, deposited thickness per process and fillet throat; diameter range for pipe.
Process and fillerISO 4063 processes in order of application, filler designation, ISO 14175 gases and ISO 14174 fluxes.
Positions and joint typeISO 6947 positions, joint type and weld details (with or without backing, single or multi-run).
Thermal parametersType of current, heat input, preheat, interpass temperature and post-weld heat treatment.
Test planRequired destructive and non-destructive tests, hardness limit and impact acceptance criterion.
From test piece to WPQR

A three-step flow from the pWPS and the welded test piece to a reviewed qualification record ready to be signed.

01

Start from the pWPS

Enter the preliminary specification and test piece data: material, thicknesses, joint type, position and processes.

02

Record the actual parameters

Record the welding parameters of each run, the filler, gases, preheat and the heat treatment applied.

03

Review ranges and tests

Check the calculated range of qualification and the test plan, and prepare the record for the examiner's assessment and signature.

Watch it in action: WPQR and WPS step by step

A complete walkthrough of an EN ISO 15614-1 procedure qualification, from the test piece data to the WPQR and WPS PDFs.

Watch on YouTube →

Watch it in action: ASME IX PQR and WPS step by step

A complete walkthrough of an ASME Section IX procedure qualification, with the ASME VIII-1 impact, preheat and PWHT checks, up to the PQR and WPS PDFs.

Watch on YouTube →

Watch it in action: AWS D1.1 PQR and WPS step by step

A complete walkthrough of an AWS D1.1/D1.1M:2025 procedure qualification: base metals, Figure 5.1 joint details, Annex B preheat, bend and Charpy V-notch tests, up to the PQR and WPS PDFs.

Watch on YouTube →

Procedure qualification plans

You pay per issued WPQR (or ASME PQR). A record with several processes counts as one. You use the same company account as in the welder modules, with separate WPQR credits. Secure card payment through Stripe and an instant VAT invoice.

Single WPQR

€39 + VAT

To qualify one specific procedure.

  • 1 final WPQR
  • Up to 3 processes per procedure
  • Ranges and test plan included
EasyDoc Welding helps prepare and manage procedure qualification records. It does not replace the welding of the test piece, the tests, the assessment or the signature required by the standard, which are the responsibility of the examiner or examining body.

Frequently asked questions about procedure qualification

What people ask most before preparing their first WPQR.

What is a WPQR?

The Welding Procedure Qualification Record. It records the welded test piece data, the actual welding parameters and the test results, and shows that the procedure produces joints with the required properties. Production WPSs are written from it, within the qualified range. In ASME IX the equivalent record is the PQR.

What is the difference between pWPS, WPQR and WPS?

The pWPS is the preliminary specification used to weld the test piece. If the tests are satisfactory, the WPQR is issued, which sets the range of qualification. WPSs are the specifications given to the shop for production and must stay within that range.

Which tests does EN ISO 15614-1 require?

It depends on the joint type, material, thickness and qualification level. They usually include visual inspection, volumetric and surface testing, transverse tensile and bend tests, macro-examination, hardness and, when required, impact tests. The module calculates the test plan for each test piece.

What is the difference between level 1 and level 2?

EN ISO 15614-1 includes two qualification levels. Level 2 is the more demanding one and is usually required by pressure equipment codes; level 1 has wider ranges and fewer essential variables. The level is set by the product or customer specification.

Does a procedure qualification expire?

The standard sets no expiry date for the WPQR: it remains valid as long as production stays within the qualified range. Some product codes or customers may impose additional requirements.

Does the software replace the examiner or examining body?

No. EasyDoc Welding helps prepare the record and calculate the ranges and the test plan, but the welding of the test piece, the tests, the assessment and the signature are carried out by the relevant examiner or body.

Can I use my WPQ module account?

Yes. It is the same company account as in the welder qualification modules EN ISO 9606-1, ASME IX and AWS D1.1. WPQRs are purchased separately, with their own credits.

Prepare your first WPQR

Start for free with the EN ISO 15614-1 module and check the range of qualification of your procedure live.